



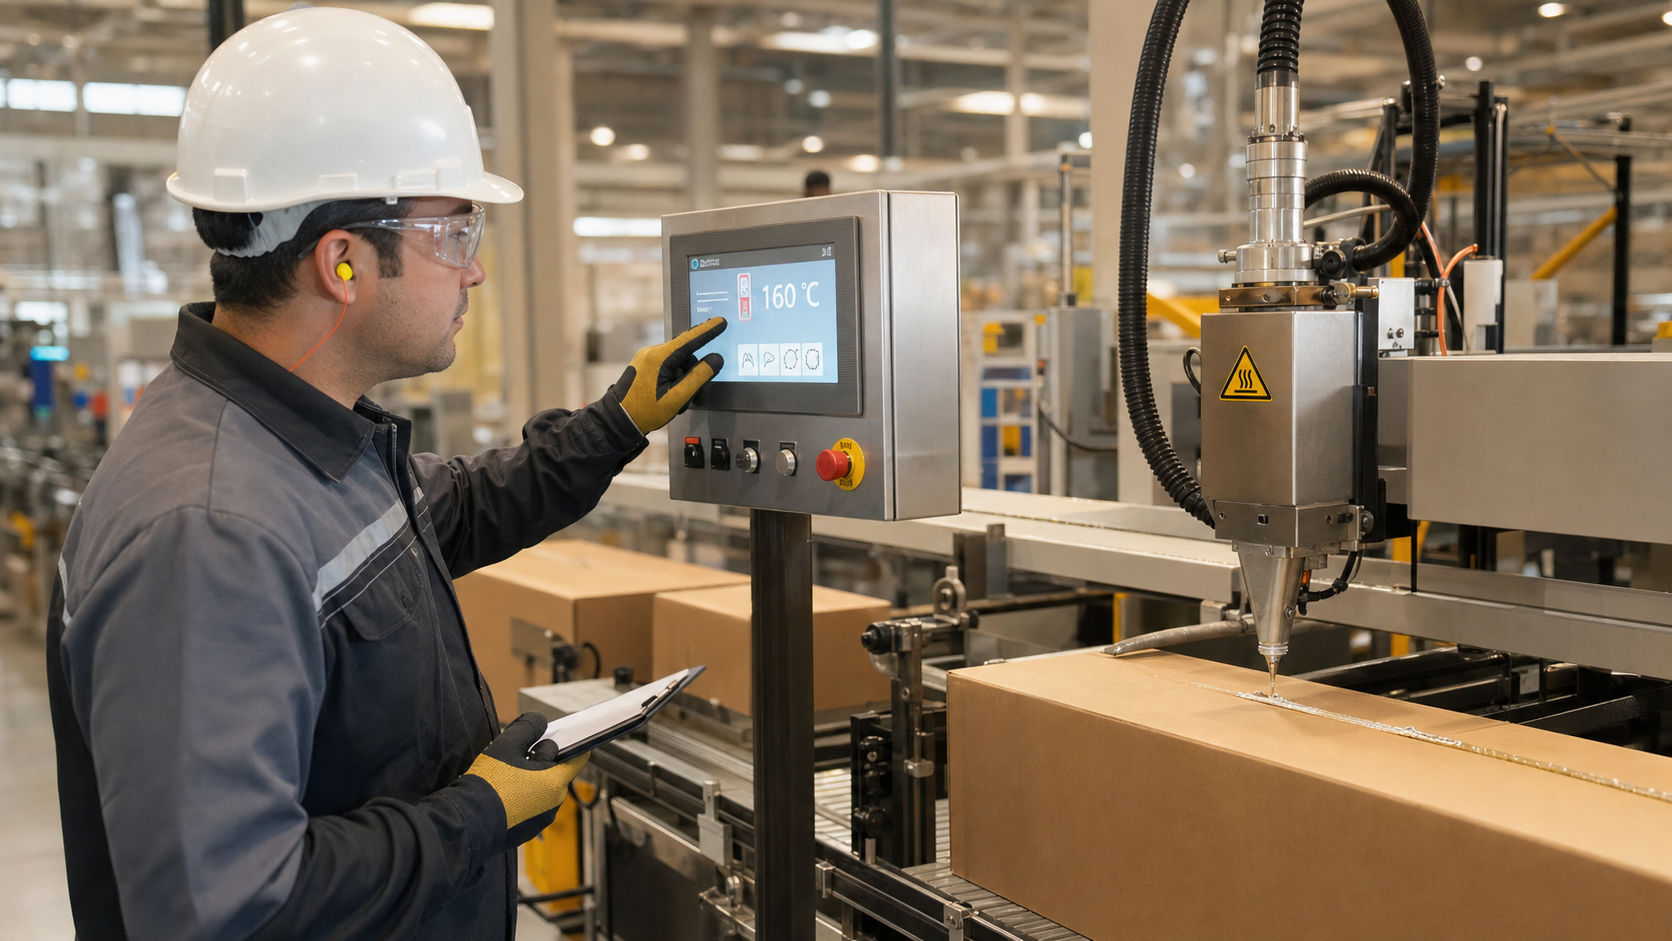
City Based Hot Melt Startup Control Card: Istanbul, Bursa and Adana Operations
The hot melt line should be opened at the beginning of the shift with trial product at low speed after the tank, hose and nozzle temperatures stabilize. Normal production speed should not be started until the glue line, adhesion break test and consumption value are verified.
Correct start on the hot melt line; It is completed when the tank, hose and nozzle temperatures stabilize, a continuous glue line is seen on the trial product and adhesion is confirmed. Businesses in Istanbul, Bursa and Adana can use the same basic control steps; Target values should be determined according to the technical sheet of the adhesive used, packaging surface and line speed.
How to handle city-based diversity?
The city name alone does not determine the process setting. Regional temperature and humidity; Ambient temperature, relative humidity and material condition should be added to the initial record as these may affect the storage conditions and surface temperature of the carton. Thus, data from Istanbul, Bursa or Adana facilities can be compared with the same method.
- Environment record: Temperature, relative humidity and the arrival time of the package from the warehouse to the line are recorded.
- Machine record: Actual temperatures of tank, hose and nozzle are checked.
- Application record: Line speed, glue amount and glue line are monitored.
- Quality record: Fiber breakage or adhesion test recommended by the manufacturer is applied.
24-hour calibration logic
| Control | First 15 min | First 60 min | 12 hours later |
|---|---|---|---|
| Temperature | Actual measurement confirmation | Trend control | Fixing decision |
| Nozzle | Is the visual line readable? | Micro clogging control | Period setting |
| Consumption | Transition difference is noted | City comparison | Increase / decrease decision |
| Record | Product, lot, shift are added | Short notes are processed | Night-control summary |
10-minute check-box
- Panel set value and actual application temperature are matched.
- The position and continuity of the glue line on the first product is checked visually.
- After product change, tank, hose, filter and nozzle flow are reviewed.
- The starting grade is carried over to the next shift.
Quick comparison on product pages
- Hot melt product guide – process targets and application ranges
- EVA hot melt – short term initial behavior
- PO hot melt (Jowatherm PO 851-10) – product transition and stability notes
- Packaging glue solutions – parcels, boxes and other packaging applications
Frequently asked short answers
- What to look for in the first 15 minutes? Temperature, consumption and visual line are read together.
- Does the threshold change in Istanbul? Yes, the intervention threshold can be relaxed depending on the daily environmental impact.
- Whose grade is insufficient? The grade is insufficient if it does not include the reason and result of the intervention.
City Based Hot Melt Startup Control Card: Istanbul, Bursa and Adana Operations hakkında merak edilenler
Why is a city-based startup plan necessary?
Intervention windows vary as the same product sees different humidity, speed and shift patterns in different cities.
How many minutes does it take to make a decision?
Temperature, nozzle behavior and consumption trend should be verified for at least the first 15 minutes.
How is product exchange handled in the first step?
The product, lot, target temperature and initial consumption value are recorded; Then the comparative testing begins.
Does the same card work day and night?
Yes. Threshold and speed tolerance differ depending on the clock range, but the same card frame can be used.
What should be extra looked for on the Bursa line?
Since the product switching frequency is high, the deviation trend in the first 20 pieces should be noted.
Who should write the note?
The shift leader initiates, the quality controller verifies the reason for the intervention and the result.
Technical resources and verification
The content has been prepared in Turkish with the technical experience of Koçak Endüstri, based on the following manufacturer resources.
Let's choose the right adhesive for your application together
You can get technical guidance and offers for Jowat products by sharing your machine, material and consumption information.
Get a technical quote

