



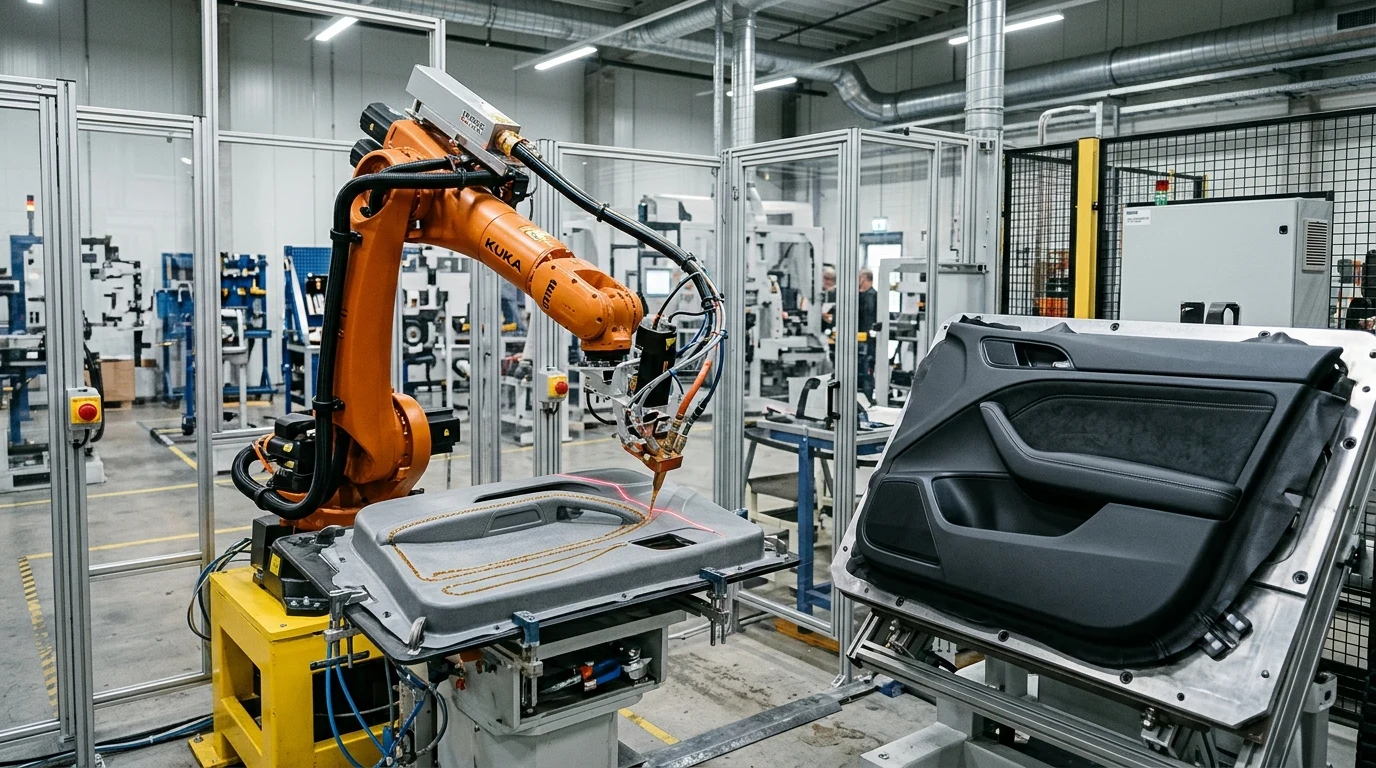
Automotive Interior Trim and Door Panel Lamination: Low Emission (VOC/FOG) Standards and PUR/PSA Selection
Adhesives in automotive door panels, headliners, and instrument panels must withstand peak interior cabin temperatures of +110°C to +120°C while complying with VDA 278 / VDA 277 limits for ultra-low VOC (Volatile Organic Compounds) and FOG (windshield fogging). Moisture-curing reactive PUR hot melts (Jowatherm-Reaktant®) form permanent thermoset cross-links meeting stringent OEM thermal creep specifications. Pressure-sensitive Mayer PSA adhesives secure acoustic felts and wire harnesses with high instant green strength.
Automotive interiors demand durable lamination of PVC synthetic leathers, TPO foils, textiles, and authentic leather onto ABS, PC/ABS, PP, or natural fiber (NFPP) substrates. These components face extreme greenhouse temperatures behind windshields, demanding compliance with strict OEM flammability, emission, and durability standards.
1. Key Engineering Criteria for Automotive Interior Trim Lamination
Under direct solar radiation, cabin temperatures on door upper trims and dashboards can reach +115°C to +120°C. Thermoplastic glues soften under this load, causing unsightly trim delamination. Global OEMs and Tier-1 suppliers therefore mandate reactive polyurethane (PUR) hot melt adhesives for permanent interior bonding.
2. OEM Standards: VDA 278, VOC, and FOG Thresholds
- VOC (Volatile Organic Compounds - VDA 278): Outgassing emissions released into the vehicle cabin. Stringent limits have completely eliminated solvent adhesives.
- FOG (Condensable Fogging - VDA 278 / DIN 75201): Heavy hydrocarbon condensates that deposit an oily haze on the windshield, compromising driving visibility.
- Odor Evaluation (VDA 270): Human sensory panel tests to ensure adhesives do not emit unpleasant odors inside the passenger compartment.
3. Reactive PUR Hot Melt: Superior Heat and Aging Performance
Reactive PUR hot melts are applied molten at 120°C–140°C. Following part compression, the prepolymer cross-links with ambient humidity into an infusible thermoset matrix:
- Withstands thermal cycles from -40°C to +130°C with zero creep.
- Resistant to high relative humidity, temperature shocks, and hydrolysis.
- Forms an effective barrier against plasticizer migration from synthetic leather.
7. Frequently Asked Questions (FAQ)
For technical consultations or OEM product specifications, reach out to the Koçak Endüstri automotive specialists.
Automotive Interior Trim and Door Panel Lamination: Low Emission (VOC/FOG) Standards and PUR/PSA Selection hakkında merak edilenler
Why is PUR hot melt mandatory for automotive door panels instead of EVA?
In-cabin summer temperatures can exceed 110°C, causing thermoplastic EVA glues to remelt and delaminate. PUR cross-links into a thermoset bond that cannot melt or creep.
What is the VDA 278 test standard?
VDA 278 is a thermal desorption method used to quantify VOC and FOG emissions from interior automotive materials, ensuring healthy cabin air and clear windshield visibility.
Can PUR hot melt bond directly to polypropylene (PP) substrates?
PP is a low surface energy plastic. Surface pretreatment (plasma, flame, or corona) is required to raise surface energy above 38-42 mN/m before adhesive application.
How long does PUR adhesive take to fully cure?
Initial handling strength is achieved in seconds during pressing, while full moisture cross-linking completes in 24 to 72 hours.
Technical resources and verification
The content has been prepared in Turkish with the technical experience of Koçak Endüstri, based on the following manufacturer resources.
Let's choose the right adhesive for your application together
You can get technical guidance and offers for Jowat products by sharing your machine, material and consumption information.
Get a technical quote

