



Nozzle Cleaning Continuity: Gaziantep and Eskişehir Centered Control Distribution
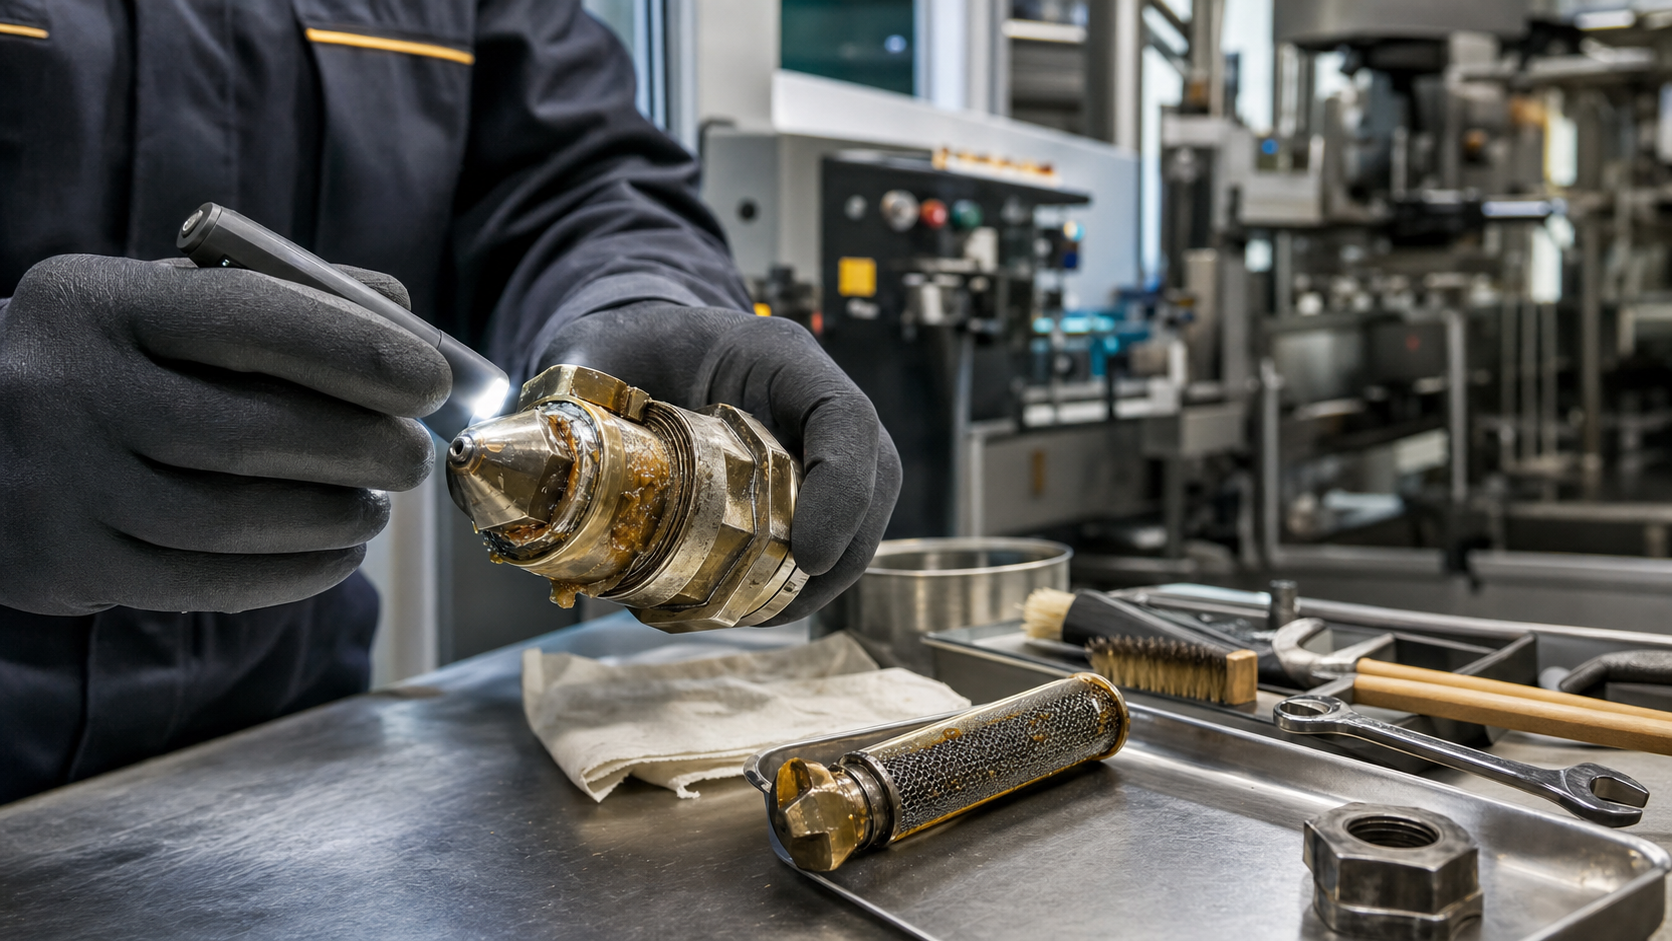
Hot melt nozzle cleaning is not according to a fixed city calendar; The adhesive used should be planned according to the working time, downtimes and changes in the glue line. When a broken or deflected line is seen, temperature and pressure should be checked, and maintenance should only be carried out after the equipment is in a safe state.
Nozzle maintenance interval is not determined solely by the elapsed time. Thermal stability of the adhesive, long downtimes, tank remaining open, filter load and change in the glue line are evaluated together. The correct approach for businesses receiving service in Gaziantep and Eskişehir is observation-based maintenance record and manufacturer's instructions.
How is city difference taken into account for cleaning?
Ambient dust can increase the risk of contamination in open tank systems; But city or climate is not the only cause of nozzle clogging. Excessive temperature, long waiting, foreign matter and unsuitable product passage should also be checked.
Practical 6-hour cycle
- Nozzle surroundings, hose connections and filter pressure are checked at the beginning of the shift.
- During production, cuts, direction changes and threading in the glue line are recorded.
- During a planned stop, the system pressure is safely released and the locking procedure is applied.
- The nozzle and filter are cleaned or replaced using the method recommended by the equipment manufacturer.
Dealing with dust or dryness
The frequency of filter monitoring and mini observation is increased.
If the open hold increases, the speed-control balance is recalibrated.
The cleaning round is triggered early after the new product.
If the night shift note is missing, correction will be made at the opening of the second shift.
Product and process matching
- EVA hot melt product details – fast initial cleaning behavior
- Jowatherm PO 256.10 – product features and application areas
- Packaging glue – surface adhesion relationship
- RIEPE product family – process support products and cleaning aids
Brief FAQ
- When is intermediate cleaning required? If consumption increase and visual fluctuation occur together.
- Critical time for Gaziantep? The first 2 hours after the product transition are considered critical.
- The most frequently forgotten thing in Eskişehir? Skipping the filter control note in hours.
- How many minutes of control is enough? It is most effective to start with mini tours that can be done in 10 to 20 minutes.
Nozzle Cleaning Continuity: Gaziantep and Eskişehir Centered Control Distribution hakkında merak edilenler
How to measure consistency in nozzle cleaning?
It is not measured as a continuous time, but over a 6-hour cycle and notes from the interaction of product + powder + speed.
Earliest alarm for Gaziantep line?
If visual deterioration comes together with increased consumption, a cleaning tour begins.
Where does the problem appear in Eskişehir?
It is seen early as increased filter noise and fluctuation in nozzle stability.
How often is cleaning performed?
It opens by following the product profile for a fixed time. If the need increases within the first two hours, the period becomes more frequent.
How long does the mini tour take?
It is usually completed in 8 to 15 minutes; If the result is fast, it closes with shift registration.
Should RIEPE always be used?
RIEPE support products are selected according to the process need; The surface and environmental behavior of each line is different.
Technical resources and verification
The content has been prepared in Turkish with the technical experience of Koçak Endüstri, based on the following manufacturer resources.
Let's choose the right adhesive for your application together
You can get technical guidance and offers for Jowat products by sharing your machine, material and consumption information.
Get a technical quote

