



What Types of Edge Banding Hot Melt Adhesive Are There?
The right edge banding adhesive depends on the panel and tape materials, machine type, line speed, application temperature, open time, required moisture and heat resistance, joint visibility and colour. EVA is a practical and economical choice, reactive PUR is considered for high ultimate durability, and PO can be preferred for specific surfaces and process requirements.
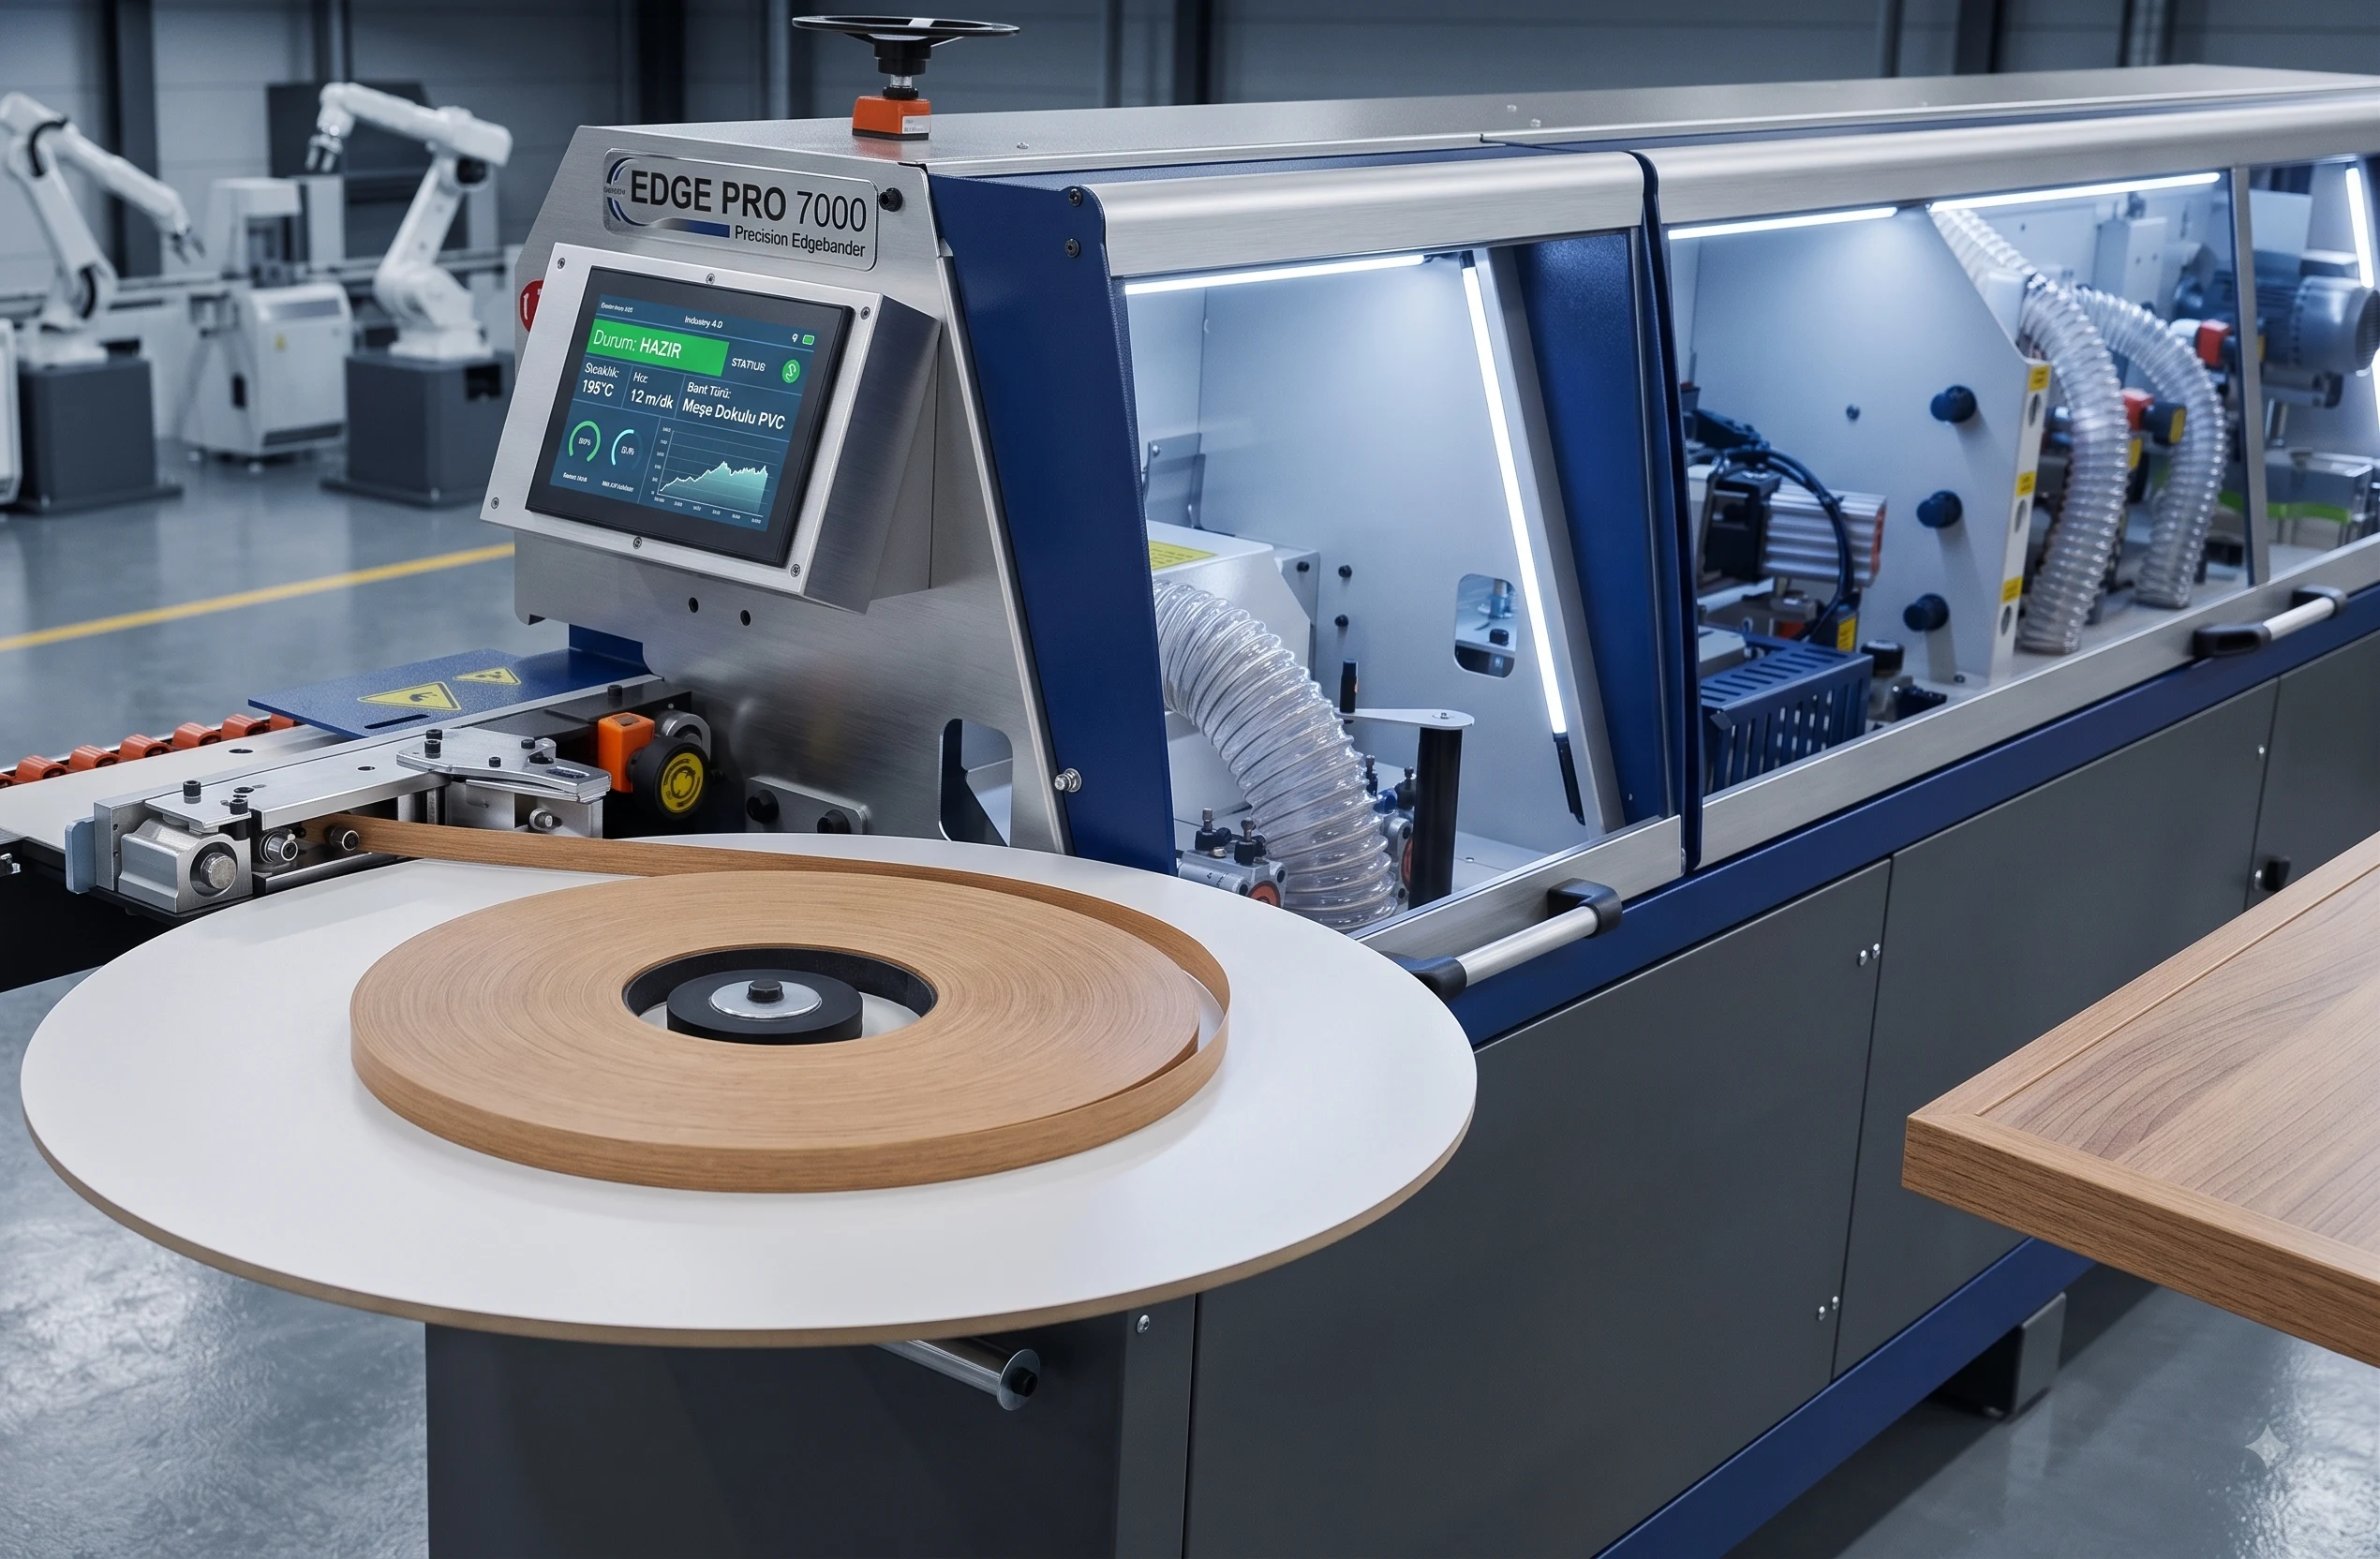
Edge banding adhesive is a hot-applied adhesive that fixes PVC, ABS, melamine or wood tape to the cut edge of MDF, chipboard, plywood and similar panels. It is usually called hot melt: the solid adhesive is melted in the heated tank of the edge banding machine and transferred between the panel and the tape.
A correct choice improves not only appearance but also resistance to impact, moisture, cleaning and temperature changes. The adhesive should therefore be selected with the tape, panel, machine speed, open time, application temperature and service conditions in mind.
What is edge banding adhesive and how does it work?
The adhesive is heated to a controlled temperature and applied by a roller, nozzle or application head. The tape is pressed onto the panel while the adhesive still has the flow and wetting needed for bonding. Cooling creates the initial hold; with reactive PUR, curing continues through a reaction with moisture.
Melting behaviour, viscosity, wetting, open time and pressing time must match the production rhythm. Before choosing a product, review the edge banding adhesive product family and the hot melt adhesive guide.
1. Types by chemical structure
The three main families used in edge banding are EVA, PUR and PO/polyolefin. These names describe technology families, not a single performance level. The current product TDS should always be checked for temperature, viscosity, open time and resistance values.
EVA edge banding adhesives
EVA (ethylene vinyl acetate) is the most common and economical thermoplastic hot melt family. It melts when heated, wets the tape and panel, and forms a physical bond as it cools. It is suitable for many standard PVC, ABS and melamine edge banding lines when the product and machine settings are matched correctly.
- Strengths: fast initial hold, broad availability, economical processing and easy changeover.
- Controls: joint visibility, open time, re-softening at heat, colour change and exposure to high moisture.
- Typical fit: standard indoor furniture and high-volume production with a stable hot melt process.
Reactive PUR hot melt adhesives
PUR (reactive polyurethane) first bonds through hot application and cooling, then continues curing by reacting with moisture in the air or substrates. Once fully cured, it can provide higher long-term resistance to moisture, water, heat and some chemicals than a conventional thermoplastic bond.
PUR may be considered for kitchens, bathrooms, commercial interiors and projects with demanding service conditions. It also requires moisture protection, a suitable machine system, controlled packaging, curing time and timely cleaning. Review the PUR adhesive product family together with these process requirements.
PO or polyolefin edge banding adhesives
PO (polyolefin) adhesives are thermoplastic hot melts with a different polymer structure from EVA. Flow, hardness, flexibility, wetting, colour and heat behaviour can therefore differ. Some PO products are selected for clean processing, stable application or specific tape and panel surfaces.
PO should not be treated as automatically better than EVA or as universally compatible with every plastic tape. The choice must be verified against the backing, panel, machine, line speed and a real sample. The general differences are also explained in the PO hot melt and EVA comparison.
| Decision point | EVA | Reactive PUR | PO / Polyolefin |
|---|---|---|---|
| Bond mechanism | Melting and cooling | Initial cooling plus moisture curing | Melting and cooling |
| Main advantage | Economical and easy to manage | High ultimate durability target | Specific surface and clean-process performance |
| Machine control | Standard hot melt equipment | Moisture-controlled and disciplined system | Correct tank, roller/nozzle and temperature window |
| Cleaning | Routine cleaning and controlled changeover | Special cleaning and timely maintenance are critical | Follow the product changeover instructions |
2. Classification by application method
Flat edge banding
Automatic straight-line machines require consistent flow, fast initial hold, a stable glue line and an open time that matches line speed. Panel temperature, tape width, application quantity, pressing and finishing stations should be assessed together. Raising temperature alone is not a reliable solution because overheating may cause degradation, odour and colour change.
Curved and special-geometry edges
Curved parts and manual or semi-automatic work have different contact and pressure times. Open time and initial tack must allow the tape to follow the radius without moving. The radius, tape thickness, backing treatment and pressing tool should be verified on a real sample.
Profile wrapping and mouldings
Profile wrapping and moulding applications need controlled wetting, initial tack, flexibility and surface compatibility over a wider or multi-sided surface. Do not assume that a product for a straight panel edge is automatically equivalent. Compare the profile wrapping adhesive solutions when the application is a profile or moulding.
3. Selection by colour and appearance
Joint appearance depends on adhesive colour, tape colour, texture, glue quantity, pressure and finishing quality. Colour alone cannot hide an excessive glue line or an uneven panel edge.
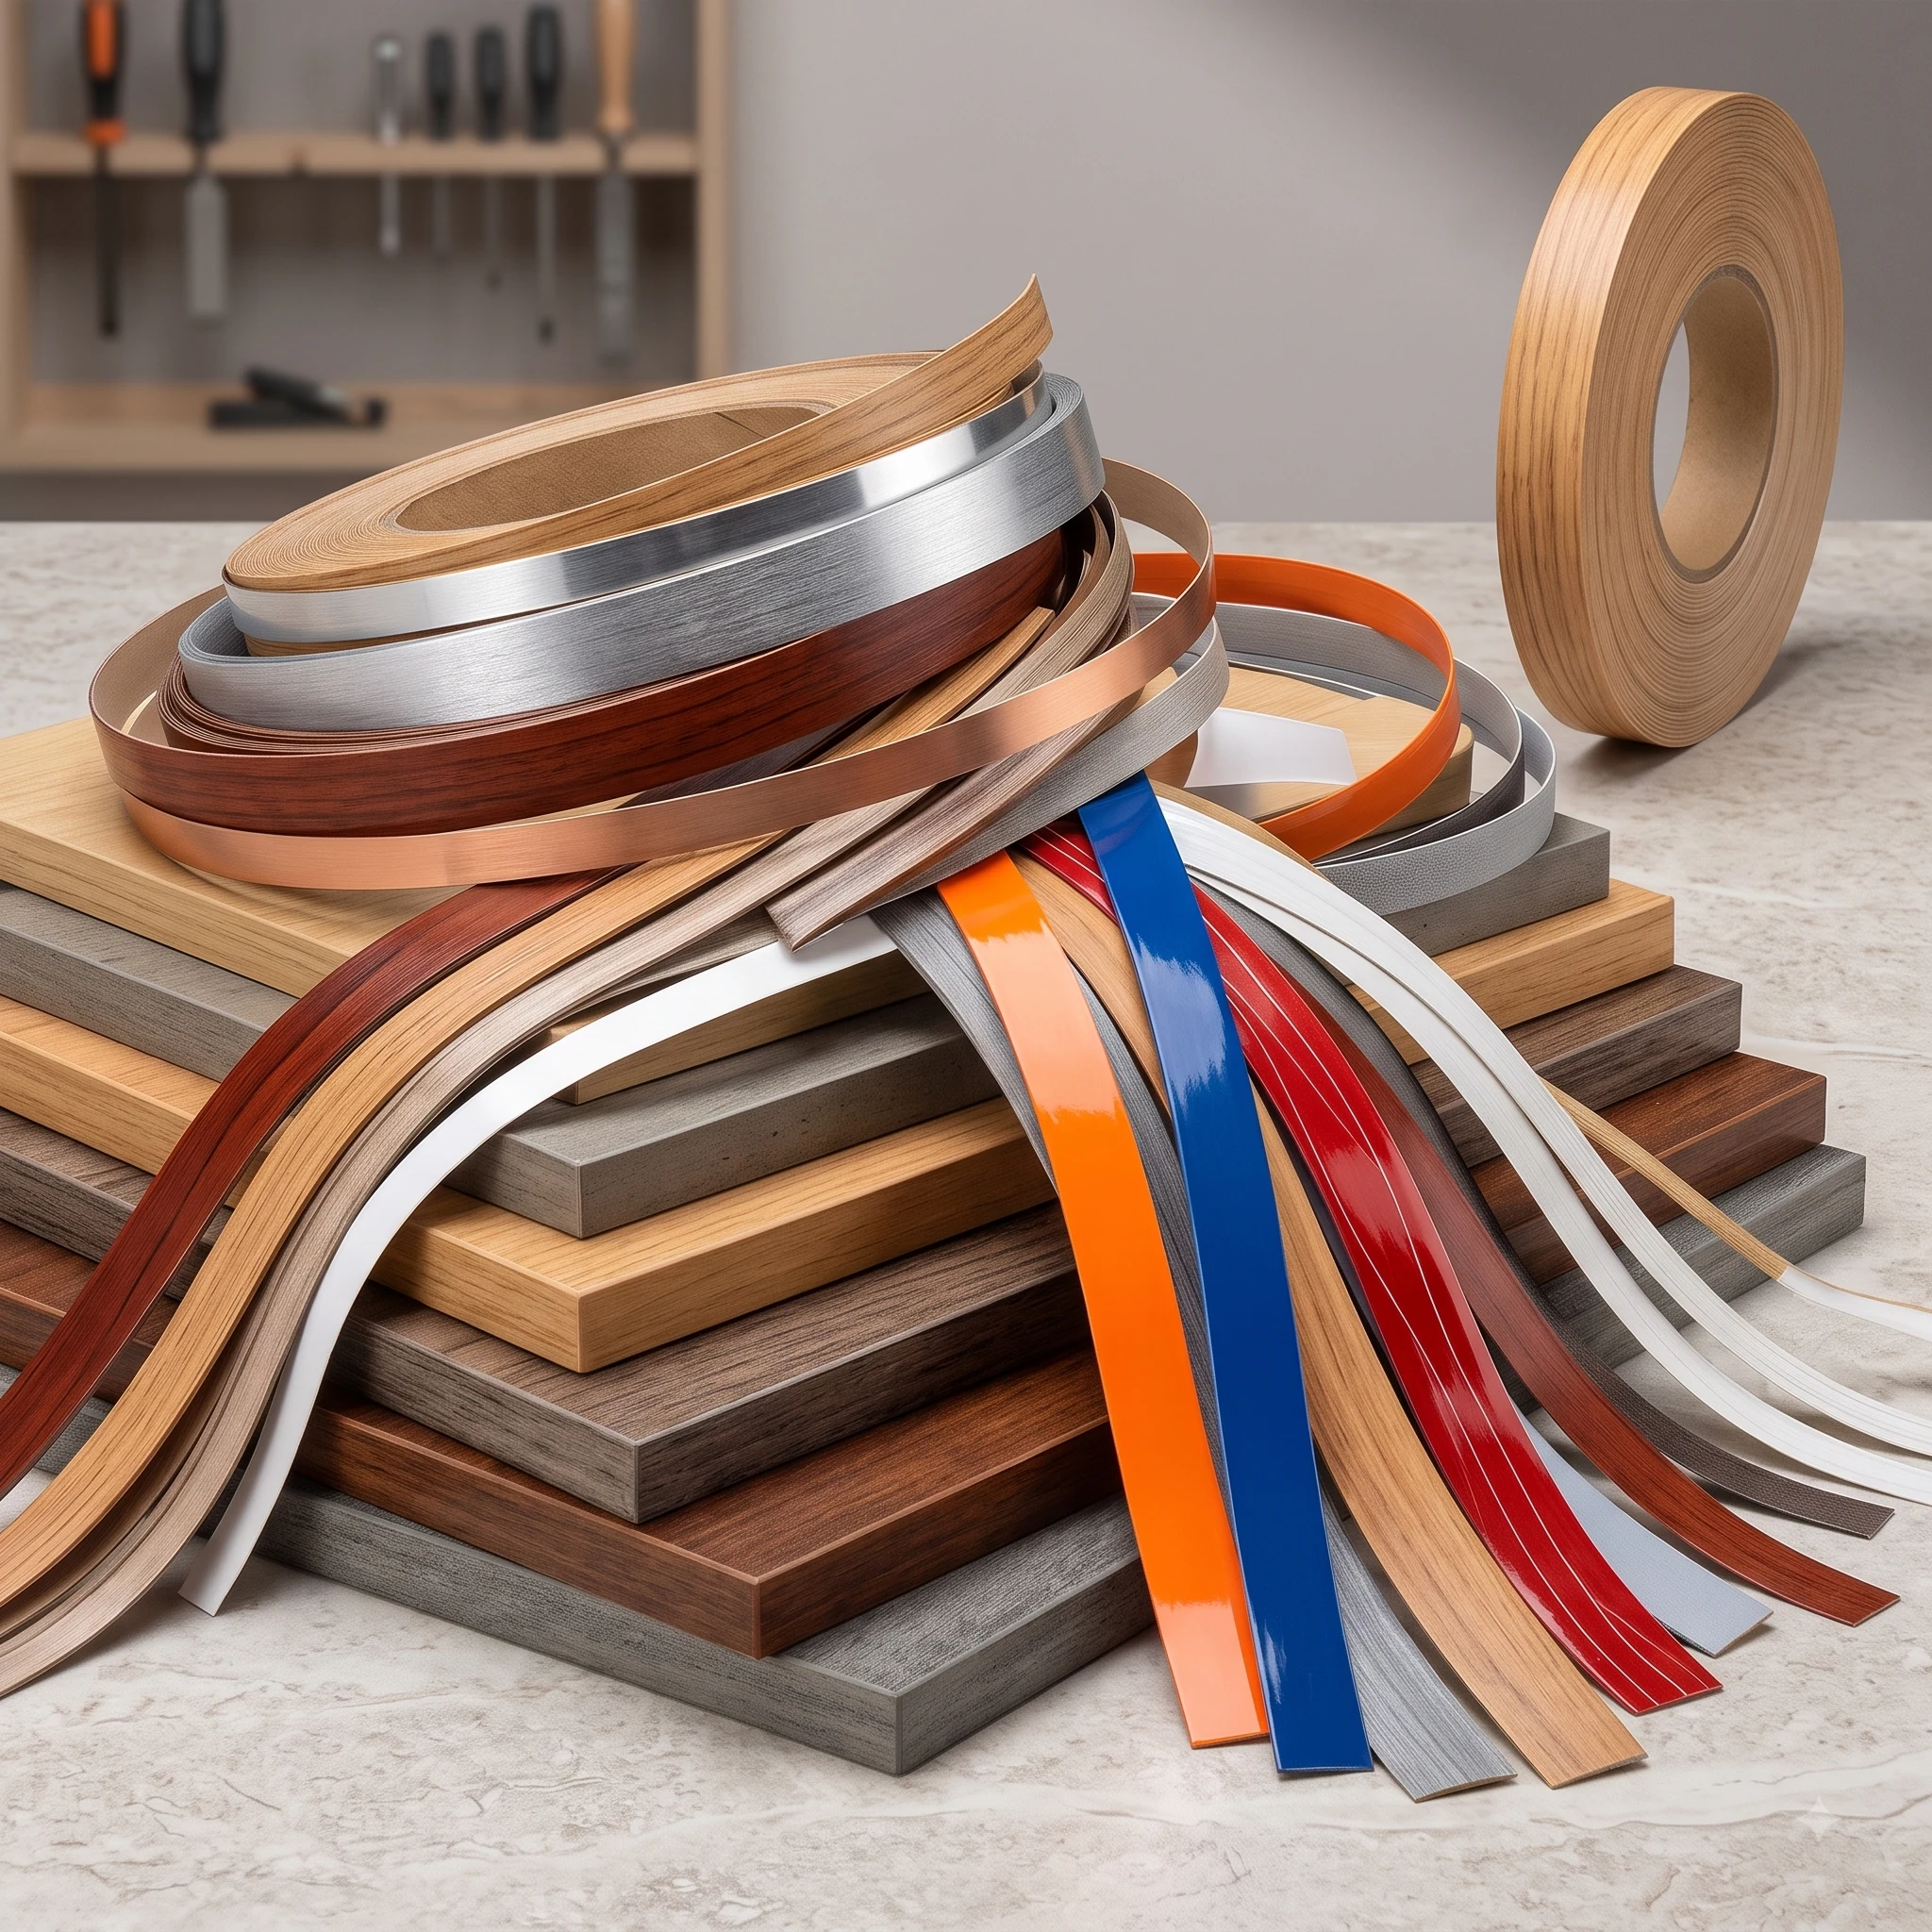
- Natural or yellowish: commonly used with woodgrain panels and warm decors.
- White: can reduce contrast on white MDF, laminate, acrylic and light-colour surfaces.
- Black or anthracite: helps reduce contrast on dark panels and tapes; residue control remains important.
- Transparent: may support a very discreet joint when the formulation, surface and process are suitable.
4. Tape and panel compatibility
Check the tape backing, primer or corona treatment, panel porosity, cut quality and surface contamination. PVC, ABS, melamine, veneer and acrylic tapes do not always have the same bonding window. A product claim such as suitable for PVC is not a substitute for a sample test on the actual panel and tape.
5. Process parameters and machine settings
Use the TDS as the starting point for tank, roller, hose and nozzle temperatures. Then control line speed, glue quantity, pressure, panel and tape temperature, open time, cooling and finishing. A stable process log makes it easier to identify whether a defect comes from the adhesive, the machine or the substrate.
6. Practical selection matrix
| Requirement | First option to evaluate | Important check |
|---|---|---|
| Economical standard indoor furniture | EVA | Joint appearance, heat window and line speed |
| High moisture and long-term durability | Reactive PUR | Moisture control, curing and cleaning |
| Specific surface or clean-process need | PO | Backing compatibility and sample result |
| Dark or light visible decor | Matching colour or transparent formulation | Glue line, dosage and finishing quality |
For a reliable decision, record the panel, tape, machine, line speed, temperature, glue quantity, joint appearance and service condition. For technical guidance and product selection, contact Koçak Endüstri.
What Types of Edge Banding Hot Melt Adhesive Are There? hakkında merak edilenler
Which edge banding adhesive is most common?
EVA is widely used in standard furniture production because it is economical, practical and compatible with many hot melt machines. The correct product still depends on the panel, tape and service conditions.
Is PUR always better than EVA?
No. PUR can offer higher ultimate moisture and heat resistance, but it requires stricter moisture control, curing and cleaning. EVA may be the more efficient choice for a suitable standard indoor process.
Can PO adhesive be used on every plastic tape?
No. PO compatibility depends on the tape backing, panel, machine settings and the specific formulation. Verify the result with the TDS and a sample test.
Which colour adhesive should be used on white panels?
White or suitable transparent products can reduce the visible contrast, but glue quantity, pressure, tape fit and finishing are equally important.
Is transparent hot melt completely invisible?
It can reduce the visual joint when the formulation and process are suitable, but no colour can compensate for poor fit, excessive dosage or an uneven edge.
What should be checked before changing adhesive?
Check the machine cleaning procedure, temperature window, viscosity, open time, tape and panel compatibility, and record the first-piece quality after changeover.
Does machine speed affect adhesive selection?
Yes. Faster lines demand compatible flow, wetting, open time and initial hold. The complete process should be tested at the real production speed.
Where can I get technical selection support?
Share the machine, panel, edge tape, speed, temperature and service conditions with Koçak Endüstri so the product family can be evaluated with a sample and current TDS.
Technical resources and verification
The content has been prepared in Turkish with the technical experience of Koçak Endüstri, based on the following manufacturer resources.
Let's choose the right adhesive for your application together
You can get technical guidance and offers for Jowat products by sharing your machine, material and consumption information.
Get a technical quote

