



Choosing Adhesive by Edge Band Material: PVC, ABS, PP, PMMA and Melamine
Adhesive selection is not based on the tape name alone. Backside treatment, panel surface, surface energy, machine speed, service environment, visible glue line and heat/moisture requirements must be considered together. EVA is often a starting option for standard work, PO for selected surface and process goals, and PUR for demanding service conditions—always confirmed by product TDS and samples.
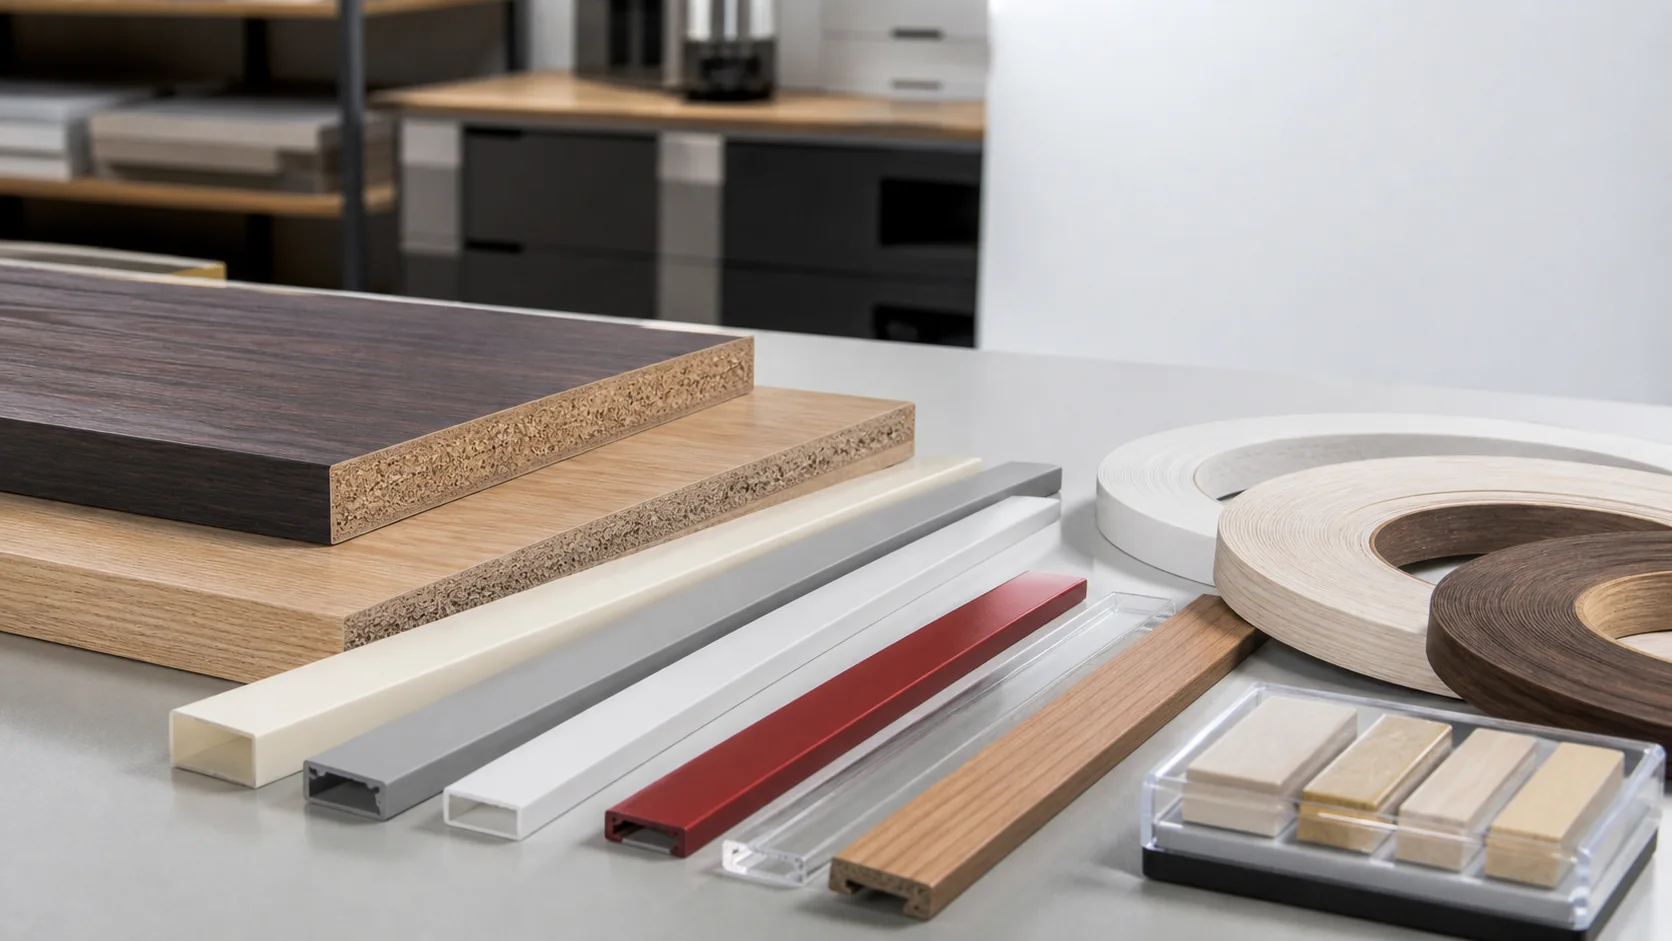
Edge banding protects the cut panel edge and defines the furniture appearance. PVC, ABS, PP, PMMA, melamine and wood bands do not have the same surface energy, stiffness, flexibility or backside preparation. A product that works on one tape may not work at the same speed and settings on another.
Selection should combine tape, panel, backside primer, line speed, temperature, pressure, service environment and appearance target. TDS values provide the starting point; a real production sample provides the final evidence.
Main edge band material differences
| Material | General consideration | Key check |
|---|---|---|
| PVC | Common thermoplastic tape with varied finishes | Backside, plasticiser effect, cleanliness and heat sensitivity |
| ABS | Impact and appearance expectations are often important | Surface fit, tape stiffness, cutting and glue line |
| PP | Lower surface energy can make adhesion verification critical | Primer/backside treatment and real sample |
| PMMA | Gloss and optical appearance are high priorities | Marks, colour, line visibility and heat effect |
| Melamine/CPL | Resin-coated or decorative paper surface | Backside structure, absorption and contact |
| Wood | Natural pores, moisture and grain variation | Moisture, surface flatness, pressure and open time |
Surface and backside compatibility
On plastic tapes, wetting depends strongly on backside primer or treatments such as corona. Increasing heat alone may not solve a low-energy PP surface; product, preparation and clean process must be verified together.
- Confirm the tape backside treatment and storage condition.
- Remove dust, oil and loose particles from panel and tape.
- Use close-up samples for glossy surfaces and visible glue lines.
- Test adhesion after heat, moisture and ageing exposure when required.
Choosing EVA, PO and PUR
EVA hot melt is a common and economical starting option for standard edge banding. PO hot melt may be assessed for clean process, colour/heat stability and selected surface compatibility. Reactive PUR hot melt may be considered when final bond strength, moisture or heat resistance is important, but it requires moisture control, closed-system discipline and special cleaning.
Compare the technologies in the EVA, PO and PUR decision matrix and the edge band hot melt guide.
Material–adhesive matrix
| Priority | Starting approach | Sample result |
|---|---|---|
| Standard series production | Suitable EVA or PO candidate | Initial bond, line, consumption and glue line |
| Low-energy surface | Product compatible with backside treatment | Peel/strength and opening behaviour |
| Heat/moisture service | Suitable PUR or high-resistance candidate | Ageing, moisture and temperature cycle |
| Low visible glue line | Confirmed colour, viscosity and film fit | Close-up appearance and squeeze-out |
| High line speed | Compatible open time and process window | Alignment, setting and stringing |
Samples and quality control
- Record tape, panel, adhesive and machine settings.
- Check glue line, squeeze-out, alignment and surface marks on the first piece.
- Apply a suitable peel, pull or cut test to the real production sample.
- Plan a second check after moisture, heat or ageing exposure.
- Compare both first-piece and stable-production samples after a changeover.
Review Jowat product cards, Mayer product cards and the Technical Information Centre for product-specific data.
Choosing Adhesive by Edge Band Material: PVC, ABS, PP, PMMA and Melamine hakkında merak edilenler
Which adhesive is used for PVC edge banding?
EVA, PO or PUR may be evaluated depending on backside treatment, speed, service environment and the product TDS.
Does increasing heat solve PP edge band adhesion?
Not necessarily. Backside treatment, primer, cleaning and surface compatibility may be more important for low-energy PP.
How can a visible PMMA glue line be reduced?
Check colour and viscosity, controlled coat weight, tape-panel contact and clean finishing with a close-up sample.
When should PUR edge band adhesive be considered?
When final bond, moisture or heat resistance is important, subject to product-specific equipment, moisture and cleaning requirements.
Why is backside primer important?
It can affect wetting and bond formation on the tape. Confirm the treatment with the tape supplier and real samples.
Which is best, EVA, PO or PUR?
There is no universal best choice. Surface, line, service, appearance, maintenance and total cost must be evaluated together.
Technical resources and verification
The content has been prepared in Turkish with the technical experience of Koçak Endüstri, based on the following manufacturer resources.
Let's choose the right adhesive for your application together
You can get technical guidance and offers for Jowat products by sharing your machine, material and consumption information.
Get a technical quote

