



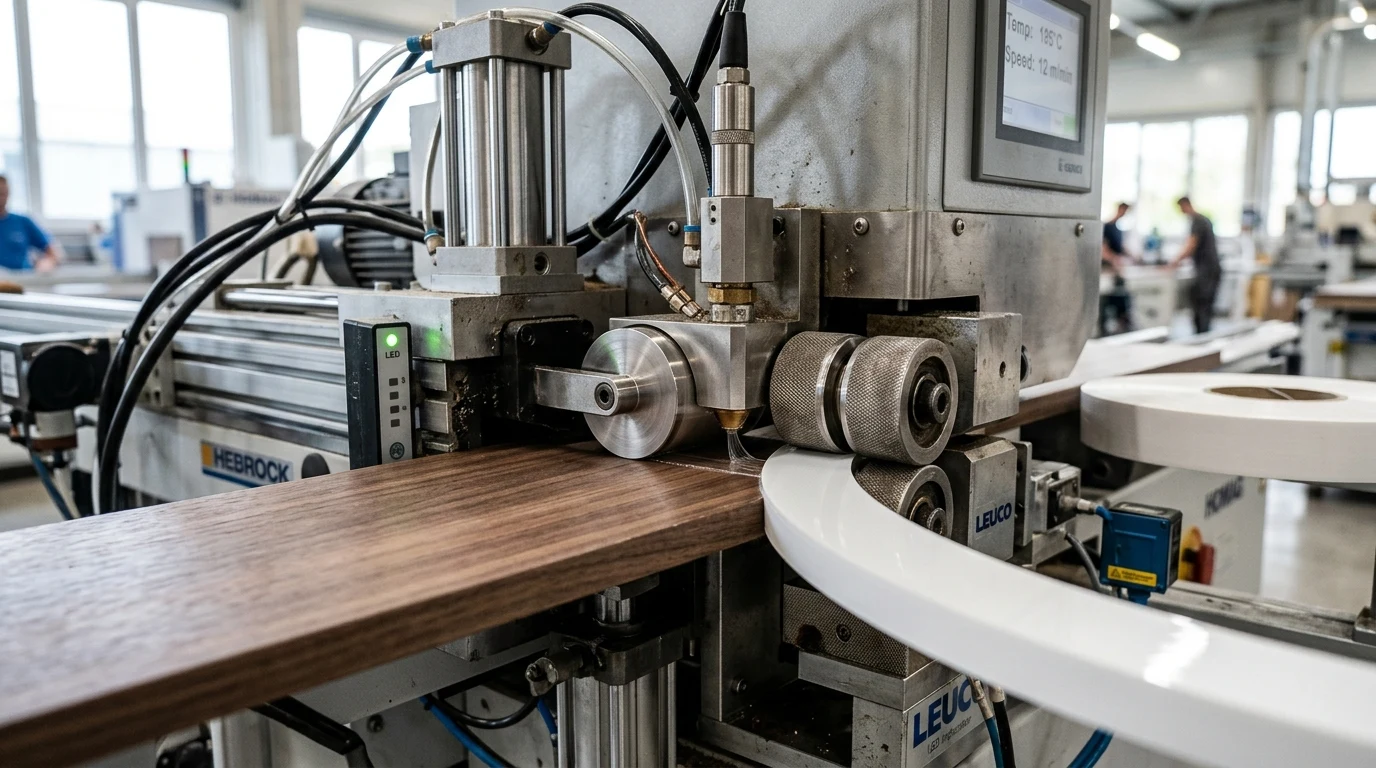
Jowat PUR Edge Banding Glue Selection and Maintenance Guide: EVA to PUR Switching, Temperature and Nozzle Cleaning
Jowat PUR edge banding glue is a reactive polyurethane adhesive that is resistant to moisture and heat (between -40°C and +140°C) and forms cross-links when exposed to moisture. It provides 'zero gap' (invisible glue line) with a much thinner film layer than standard EVA glues. When switching from EVA to PUR, the glue pot should be completely emptied and intermediate cleaning granule should be applied; During production stops, the reaction should be neutralized with a PUR cleaning kit (blue spülmittel).
Aesthetic and durability expectations in modern furniture, bathroom-kitchen cabinets and commercial interior panels have made reactive polyurethane (PUR) technology standard in edge banding processes. Jowat PUR edge banding adhesives (Jowatherm-Reaktant® product line) react chemically with moisture in the air and on the panel to form an insoluble and insoluble cross-link that exceeds the mechanical adhesion offered by thermoplastic adhesives.
1. What is Jowat PUR Hot Melt and how is it different from EVA?
Classic EVA (Ethylene Vinyl Acetate) hot melt adhesives are thermoplastic polymers that melt with heat and physically solidify when cooled. Although these systems provide cost and ease of application, they may soften at temperatures above 70°C–80°C or in intense steam/water contact, causing the edge band to open.
In contrast, Jowat PUR (Polyurethane Reagent) hot melt exhibits a two-stage bonding mechanism:
- Physical Initial Adhesion: When applied as hot melt with a roller or nozzle between 120°C and 140°C, it cools rapidly and provides a strong mechanical adhesion within seconds. In this way, the panel can immediately enter the sizing or milling line.
- Chemical Cross-linking: Within 24 to 72 hours following the application, the adhesive molecules react with the moisture in the pores of the wood panel and the ambient air. The resulting polyurethane network structure makes the glue line thermoset; It no longer melts again when heated and is insoluble in solvents.
2. Balance of Application Temperature, Viscosity and Line Speed
To maintain the chemical stability of PUR adhesives, application temperature limits must be strictly observed. Excessive temperature triggers premature reaction and viscosity increase in the glue pot, while low temperature causes insufficient wetting on the panel surface:
| Parameter | Recommended Range | Technical Impact and Critical Risk |
|---|---|---|
| Melting Tank Temperature | 120°C – 140°C | Going above 150°C rapidly increases the viscosity and initiates gelation in the glue tank. |
| Application Roller / Nozzle | 130°C – 150°C | Provides correct fluidity and film thickness at the panel contact point. |
| Application Amount (Weight) | 100 – 160 g/m² | Full strength is achieved with approximately 40% lower weight compared to EVA glues (180–250 g/m²). |
| Line Feed Speed | 15 – 35 m/min | At high line speeds, nozzle geometry and open time tolerance must be taken into account. |
| Panel Surface Temperature | Min. 18°C | Cold panel causes premature freezing of the glue ('cold check') and poor adhesion. |
3. How to Achieve Zero-Joint Edge Banding?
In the furniture industry, the term 'zero-joint' refers to the glue line between the panel surface and the ABS/PVC/acrylic edge band being so thin that it cannot be distinguished by the human eye. As an alternative to laser or hot air taping systems, correctly adjusted Jowat PUR technology offers a perfect zero-gap surface with a cost advantage:
- Precision Pre-Milling: Saw marks and microscopic breaks on the panel edge must be completely cleaned with a dual-motor diamond pre-milling cutter.
- Micro-Dosing Roller or Nozzle: The glue film should be thinned to a thickness of 0.05 mm with a slot nozzle (slit applicator) or a counter-rotating glue roller.
- Riepe® Pre- and Post-Process Chemicals: Riepe antistatic release agent applied before the glue pot prevents glue adhesion to the panel surface; The cleaning fluid before polishing removes microscopic overflows, leaving a bright and clean corner.
- Optimum Press Roller Setting: The main press roller and stepped tapered side rollers must lock the edgebanding to the panel core with millimetric pressure before the glue cools.
4. EVA to PUR Transition and Line Preparation Protocol
When switching a standard edge banding machine using EVA to Jowat PUR glue, mixing of the two chemicals in the tank should be strictly prevented. EVA and PUR residues disrupt each other's reaction balance:
- Completely Empty the EVA Tank: Drain the existing EVA glue at high temperature, scrape the tank walls with Teflon compatible apparatus.
- Apply Cleaning Granule: Bind and drain the last traces of EVA from the chamber with standard hot melt cleaner.
- Connect PUR Preheater or Cartridge System: Integrate 2 kg or 20 kg airtight Jowat PUR packages directly into the system. Use a dry air or nitrogen-protected cover that provides a moisture barrier.
- Initial Filling and Flushing (Flush): Melt the new Jowat PUR glue and flow approximately 200–300 grams through the system, removing all old chemical residue from the roller and hose.
5. Daily and Weekly Maintenance: PUR Cleaning Granule (Spülmittel)
Reactive polyurethane adhesives begin to cure as soon as they come into contact with air. Melting a PUR mass that has completely frozen in the tank or nozzle is physically impossible and requires complete disassembly and incineration or replacement of the unit. That's why disciplined cleaning protocol is mandatory:
- Short Term Stoppages (Overnight): Glue pot temperature should be reduced to 100°C or the lid of the tank should be sealed with a dry air wick.
- Weekend and Long Downtimes (Over 48 Hours): The remaining PUR glue should be drained, then the special neutralizer Jowat PUR Cleaning Granule (Blue Spülmittel) should be loaded into the chamber.
- Reaction Neutralization: After the blue cleaning granule melts, it is passed through rollers and nozzles and all reactive isocyanate groups along the line are chemically passivated. When the system cools down, this granule remains like an inert paraffin and does not damage the machine.
- Restart: When the machine is restarted, the blue granule is melted and discharged, fresh PUR glue is loaded and circulated for a few minutes until clear flow is seen.
6. Jowat Edgebanding Adhesives Comparison Matrix
| Feature | Jowat EVA Hot Melt | Jowat PO (Polyolefin) | Jowat PUR (Jowatherm-Reaktant®) |
|---|---|---|---|
| Chemical Structure | Thermoplastic Copolymer | Thermoplastic Polyolefin | Moisture Reactive Polyurethane (Thermoset) |
| Thermal Resistance | -10°C to +75°C | -20°C to +110°C | -40°C to +140°C |
| Water and Steam Resistance | Low (Risk of opening in bathroom/kitchen) | Medium - High | Full Waterproof (Steam and moisture resistance) |
| Glue Line Thickness | Prominent (0.15 – 0.30 mm) | Thin (0.10 – 0.15 mm) | Zero Gap (0.05 – 0.10 mm micro film) |
| Application Temperature | 180°C – 200°C | 170°C – 190°C | 120°C – 140°C (Low energy consumption) |
| Maintenance Requirement | Standard | Low (No carbonization) | High (Special cleaning spülmittel is mandatory) |
Switch to Jowat PUR Technology in Your Line
Koçak Endüstri technical experts perform PUR compliance audits of your existing edge banding machines, optimize your nozzle/roller settings and maximize your line efficiency with Jowatherm-Reaktant® products.
Get Technical Consultancy and Quote or View Our Jowat Product Catalog .
Jowat PUR Edge Banding Glue Selection and Maintenance Guide: EVA to PUR Switching, Temperature and Nozzle Cleaning hakkında merak edilenler
Why does Jowat PUR edgebanding glue provide zero gap?
Jowat PUR reactive adhesives create a micron-level film layer with a thickness of 0.05 mm in very low weights such as 100-140 g/m², creating an invisible connection line between the panel core and the edge band.
How should the machine using PUR glue be left on the weekend?
The container containing PUR glue must be emptied and the reaction neutralizer Jowat blue cleaning granule (spülmittel) must be loaded into the system and melted. The cleaning agent flowing through the roller passivates the isocyanate groups and prevents the unit from freezing.
Is machine modification required when switching from EVA glue to PUR glue?
Many modern edgebanding machines are suitable for direct PUR use with a teflon-lined pot or a ready-made PUR cartridge slot. In older machines, the glue pot may need to be coated with Teflon or a nozzle adapter kit may need to be installed.
How long is the full curing time of PUR glue?
PUR glues provide mechanical adhesion in seconds and the panel can be processed. Chemical cross-linking and final heat-water resistance are completed within 24 to 72 hours, depending on ambient humidity.
At what temperature is Jowat PUR glue applied?
Jowat PUR edgebanding adhesives generally work at low application temperatures between 120°C and 140°C. Temperatures above 150°C should be avoided as they may cause premature reaction and gelation in the pot.
Technical resources and verification
The content has been prepared in Turkish with the technical experience of Koçak Endüstri, based on the following manufacturer resources.
Let's choose the right adhesive for your application together
You can get technical guidance and offers for Jowat products by sharing your machine, material and consumption information.
Get a technical quote

